leave a message

How to Choose a Casting Cutting Machine?

Choosing the right Casting Cutting Machine can determine whether a foundry gains efficiency or loses hours to rework. The decision should begin with the casting itself, not the machine catalogue. Alloy hardness, wall thickness, runner size, production volume, and required surface quality all matter.

John Campbell, a respected casting authority and author of Castings, wrote, “The quality of a casting is determined by the way it is filled.” His principle also applies to cutting. A poorly planned cutting operation can introduce vibration, uneven edges, excessive dust, or avoidable material loss. The machine must therefore match the casting process from start to finish.

Look closely at the working area. Can the table support a heavy iron casting without movement? Does the cutting head reach narrow gates and awkward risers? A water-cooled blade may suit heat-sensitive work, while a robust abrasive system may perform better on thick sections. Automatic feed control can improve consistency, but it may add complexity and maintenance costs.

Small details matter.

Operators should test blade life, guarding, noise levels, extraction performance, and spare-part availability. A machine that cuts quickly but stops often is not truly productive. Energy use also deserves attention, especially during long production shifts.

There is no universal best choice. That is the uncomfortable part. A cheaper machine may appear practical, yet its limited adjustment range could restrict future orders. Conversely, advanced automation may be wasteful for low-volume work. The strongest decision combines measured trials, operator experience, supplier support, and honest cost analysis. A reliable Casting Cutting Machine should improve safety, repeatability, and output without creating new problems.
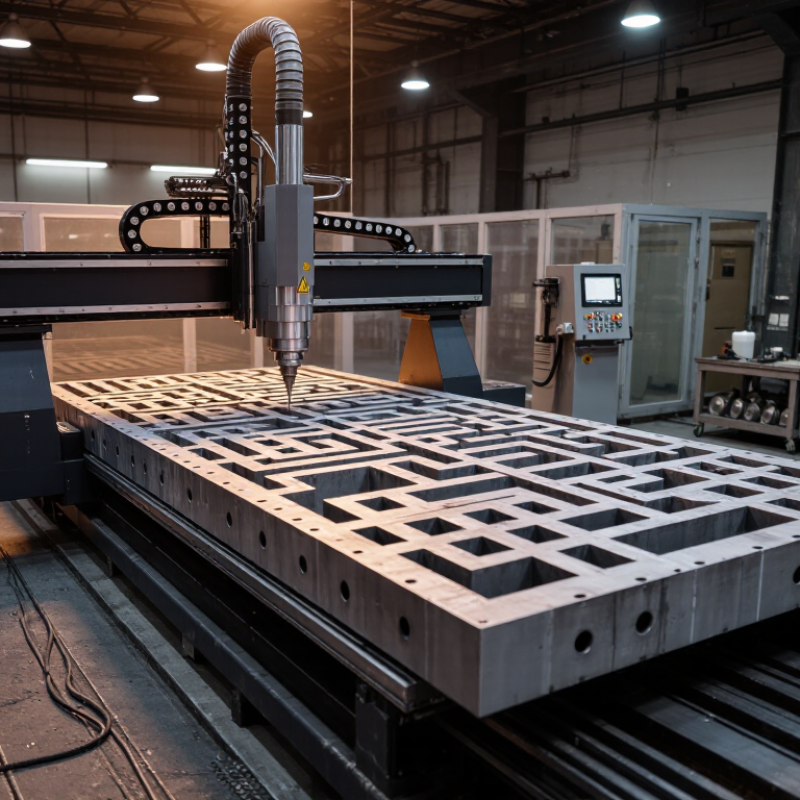
How to Choose a Casting Cutting Machine?

Define Casting Type, Section Size, and Output Target in kg/h

How to Choose a Casting Cutting Machine?

Define the casting type before comparing machine specifications. Sand castings often carry gates, risers, and uneven surfaces. Investment castings usually need cleaner, more controlled separation. Die castings may require high repeatability and careful burr control. Continuous cast products demand stable feeding and long-duty operation. The American Foundry Society’s 2023 Metalcasting Industry Census reported U.S. metalcasting shipments above 44 billion dollars in 2022. This scale shows why one machine rarely suits every casting family.

Measure the largest section size, not the average part. Record length, width, wall thickness, alloy, hardness, and gate geometry. A 120 mm riser can overload a machine designed around a 70 mm section. Cutting speed also changes with aluminum, ductile iron, steel, or heat-resistant alloys. Then define the output target in kilograms per hour. Include part weight, scrap, loading time, blade changes, and realistic machine utilization. World Steel Association data recorded 1.892 billion tonnes of crude steel production in 2023, confirming the importance of productive, durable cutting systems across heavy industry.

A neat spreadsheet can still lie. During trials, weigh complete cut cycles, not only running time. For example, 18 castings at 6 kg each, completed in 30 minutes, equal 216 kg/h before interruptions. After loading delays and maintenance, the practical rate may fall below 170 kg/h. Leave capacity headroom, but avoid buying excessive power for occasional work. Industry reports provide context; your own casting samples provide stronger evidence.
Match Wheel Diameter and the 80 m/s Rated Speed to Cut Depth

How to Choose a Casting Cutting Machine?

Wheel diameter should follow the required cut depth, not appearance. A 300 mm wheel offers roughly 150 mm of radial reach before accounting for the arbor and guard. Real cutting depth is smaller. Flanges, casting shape, and wheel wear reduce it further. A larger wheel is not automatically better. It may increase machine weight and handling effort. The Federation of European Producers of Abrasives states that reinforced cutting wheels can be rated up to 80 m/s under applicable safety guidance. EN 12413 also requires clear wheel specifications and safe operating limits.

Use this formula to check spindle speed:

RPM = 60 × 80 ÷ π × wheel diameter in metres.

A 300 mm wheel reaches about 5,100 RPM at 80 m/s. A 400 mm wheel reaches about 3,820 RPM. The machine spindle must never exceed the wheel’s marked maximum speed. The 80 m/s figure is a ceiling, not a cutting target. Lower speeds can reduce heat, vibration, and edge damage, though cutting may become slower. This balance is often overlooked.

Tips: Measure the thickest casting section first. Then select a wheel diameter with practical clearance. Check the wheel label, spindle RPM, guard size, and flange condition together.

OSHA’s abrasive-wheel requirements also emphasize guarding and compatibility. Do not trust diameter alone. In real workshops, worn wheels and uneven castings can make the planned depth imperfect. A short test cut is worth the delay.

Compare 3–15 kW Drives, Feed Rates, and Cycle-Time Data

How to Choose a Casting Cutting Machine?

Drive power should match casting size, gate thickness, and hourly demand. A 3–5 kW drive suits small aluminum gates and lighter trimming work. Medium castings often need 7.5–11 kW. Heavy gates may justify 15 kW, but higher power alone does not guarantee faster cycles. The U.S. Department of Energy reports that motor-driven systems consume roughly 70% of industrial electricity. Therefore, efficiency and load control deserve equal attention. A variable-speed drive can reduce wasted energy during return strokes and idle periods.

Feed rate must be tested with the actual alloy and cutting tool. A practical comparison might use 0.3–0.6 m/s for delicate sections, then 0.8–1.2 m/s for thicker gates. Faster feeding can shorten cutting time, yet it may increase burrs, vibration, and tool wear. Keep the operator’s hand away from the process. Cycle-time data should include loading, clamping, cutting, unloading, and inspection. Otherwise, the number looks impressive but misleads.

The European Commission’s Best Available Techniques reference for foundries emphasizes energy monitoring and process control. Record at least 30 consecutive cycles, not five perfect ones. Compare average time, worst-case time, power draw, and rejected parts. A 10-second cutting cycle may become 24 seconds on the factory floor. That difference matters. My own selection rule is simple: choose the lowest-power drive that maintains stable feed, acceptable cut quality, and measurable output. Recheck that choice after three months.

How to Choose a Casting Cutting Machine? — Compare 3–15 kW Drives, Feed Rates, and Cycle-Time Data

Reference comparison for abrasive or carbide cutting systems used on non-ferrous and ferrous castings. Actual performance depends on alloy, casting geometry, gate size, blade condition, clamping, and operator settings.

Drive Power Typical Cutting Application Typical Blade Diameter Recommended Linear Feed Rate Typical Cut Depth per Pass Typical Cycle Time per Cut Approx. Cuts per Hour Best Fit
3 kW Small aluminum and zinc gates 250–300 mm 20–60 mm/s 40–80 mm 18–35 s 90–175
4 kW Small-to-medium non-ferrous castings 300–350 mm 25–70 mm/s 50–100 mm 16–32 s 95–185
5.5 kW Aluminum, zinc, and thin-wall iron sections 350–400 mm 30–80 mm/s 60–120 mm 14–28 s 105–215
7.5 kW Medium aluminum and ductile-iron gates 400–450 mm 35–90 mm/s 80–150 mm 12–25 s 115–250
11 kW Large castings and repeated heavy cuts 450–500 mm 40–100 mm/s 100–180 mm 10–22 s 125–300
15 kW Heavy ferrous castings and large risers 500–600 mm 45–110 mm/s 120–220 mm 9–20 s 135–330

Cycle-time values include the powered cutting motion only and exclude loading, clamping, part repositioning, slag removal, and blade changes. For safe sizing, select a drive with sufficient continuous torque and reserve capacity rather than choosing solely by peak feed rate.

Specify ISO 12100 Guards, Interlocks, and Dust Control Below 85 dB(A)

Choosing a casting cutting machine begins with risk control, not cutting speed. ISO 12100 provides a useful framework for identifying hazards and reducing them through design. Specify fixed guards around blades, belts, and rotating shafts. Openings should prevent hand access to dangerous moving parts.

Interlocked doors should stop cutting movement when opened. The machine should not restart automatically after closure. Check the stopping time during commissioning, because a delayed stop can defeat an otherwise sound guard. Emergency-stop devices must remain reachable from normal working positions. They should not replace proper guarding. Small oversights matter.

Dust control needs equal attention. Ask for local extraction at the cutting point, sealed transfer areas, and a cleanable collection system. Fine casting dust can settle on floors, motors, and control cabinets. Test airflow with the machine loaded, not only when it runs empty. A visible cloud means the system needs correction.

Noise should remain below 85 dB(A) at the operator’s position under realistic production conditions. Request documented measurements, including the microphone location and operating cycle. Enclosures may reduce noise, but they can trap heat or obstruct maintenance. That trade-off deserves review.

In practice, specifications are sometimes accepted too quickly. Recheck them during installation, after tool wear, and when extraction filters become dirty. Safety is not finished when the purchase order is signed.

Evaluate Tolerance, Scrap Rate, and a 12–24-Month Payback Period

How to Choose a Casting Cutting Machine?

A suitable casting cutting machine should match your real production tolerance, not only its advertised capacity. Measure dimensional variation across several shifts, including cold starts and tool changes. In production reviews, I compare the required tolerance with actual cut samples from different operators. A machine may appear precise in a trial, yet perform differently after hours of continuous work. Small deviations can create grinding, rework, or rejected castings.

Scrap rate deserves equal attention. Record current losses by part number, defect type, and machine setting. Then estimate how much waste the new process can realistically remove. Do not assume every saved casting becomes profit. Labor, finishing, maintenance, energy, and inspection costs also affect the result. The first estimate is rarely right. Recheck it after a pilot run. A practical payback target is 12–24 months, based on verified savings rather than optimistic output claims.

Tips: Request sample cuts using your own castings. Check edge condition, cycle time, noise, chip control, and operator access. Ask for service response times and spare-part availability. Use a simple calculation: machine cost divided by monthly net savings. If the figure exceeds 24 months, review utilization, scrap assumptions, and labor requirements. Leave room for mistakes. Real factories are never perfectly predictable.

How to Choose a Casting Cutting Machine?

Evaluate dimensional tolerance, scrap rate, and the target 12–24-month payback period before selecting a cutting solution.

How to read this chart: A tighter tolerance and lower scrap rate improve part consistency and material yield. In this planning benchmark, the standard hydraulic and servo-controlled options fall within the preferred 12–24-month payback window. The high-precision automated option achieves the best process capability, but its longer payback period should be justified by high production volume or strict quality requirements.